We produce durable, efficient, and innovative machines.
-
Esenyurt / İstanbul


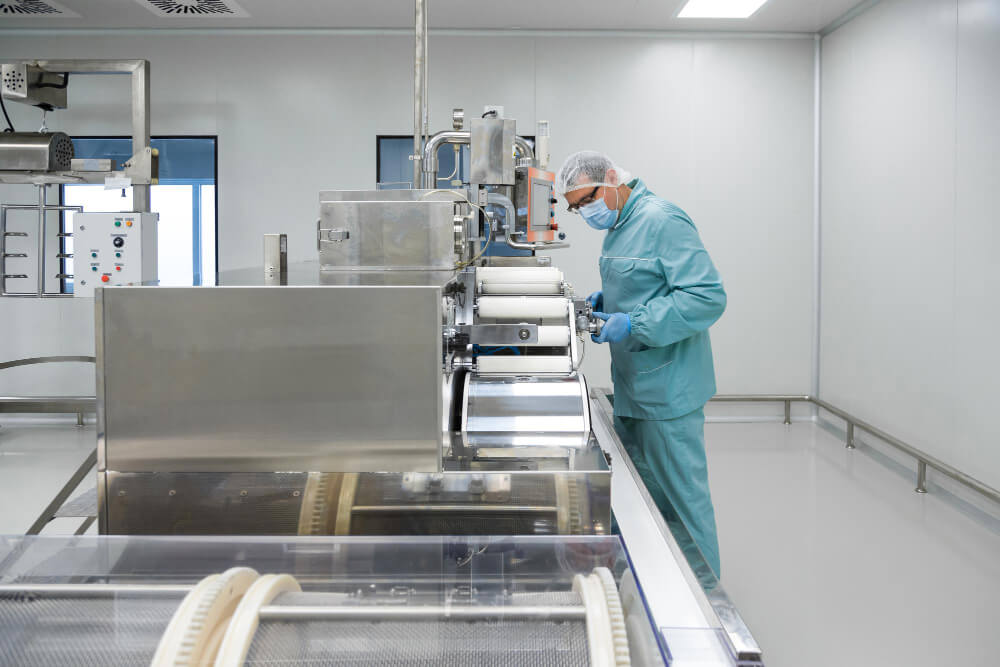
Stainless Steel Conveyor System Manufacturer for the Food Industry
In food production facilities, hygiene, durability, and continuous production flow are the three most critical factors. Therefore, selecting a stainless steel conveyor system manufacturer for the food industry is not just a machinery investment, but a strategic decision that directly affects food safety and production efficiency. Especially in high-capacity production lines, the material quality and design standards of conveyor systems directly determine product quality.
What Is a Stainless Steel Conveyor System?
Stainless steel conveyor systems are transport systems manufactured from AISI 304 or AISI 316 grade stainless steel to meet hygiene standards in food production environments. These systems ensure that products are safely, quickly, and consistently transported along the production line.
In particular, food-grade stainless steel conveyor systems play a critical role in food safety due to their bacteria-resistant surface structure and easy-to-clean design.
Why Are Stainless Steel Conveyors Essential in the Food Industry?
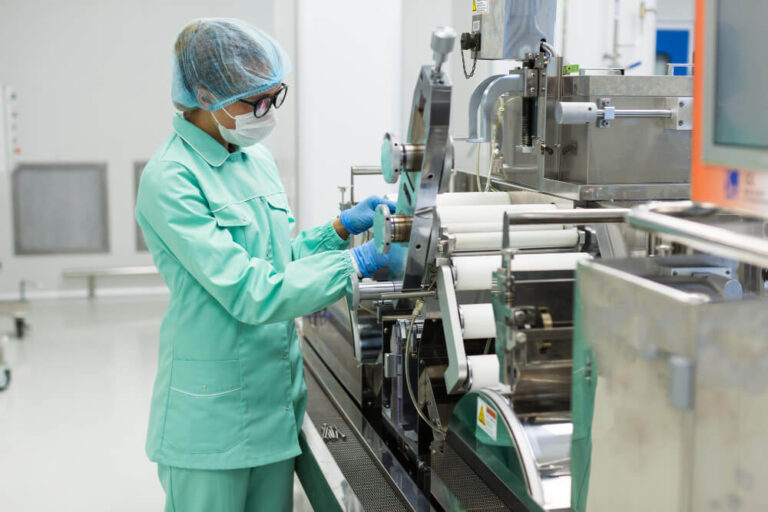
In food production, even the smallest hygiene violation can risk product quality and human health. Therefore, all equipment used must comply with food safety standards.
Stainless steel conveyor systems provide the following advantages:
- Reduce bacteria and microorganism formation
- Offer easy-to-clean surfaces
- Resistant to chemicals and moisture
- Ensure long service life
- Comply with food safety standards
In particular, hygienic food production line conveyor systems play a crucial role in compliance with HACCP and ISO 22000 standards.
Technical Features of Stainless Steel Conveyor Systems
AISI 304 and AISI 316 Stainless Steel
These are the two most commonly used stainless steel grades in the food industry.
- AISI 304: Suitable for general food production lines
- AISI 316: Preferred in environments with high salt, acid, or chemical exposure
Open Frame Design
For hygienic production, closed and hard-to-clean areas must be eliminated.
Advantages:
- Easy cleaning
- Fast maintenance
- Easy visual inspection
- Prevention of dirt accumulation
Modular Structure
Stainless steel conveyor systems are typically designed in a modular structure.
- Easy line expansion
- Component replacement flexibility
- Adaptability to production lines
Washdown-Ready System
Specifically designed for food facilities requiring intensive cleaning.
- Water and steam resistance
- Chemical cleaning compatibility
- Compliance with hygiene standards
Application Areas in the Food Industry
Stainless steel conveyor systems are used in a wide range of industries.
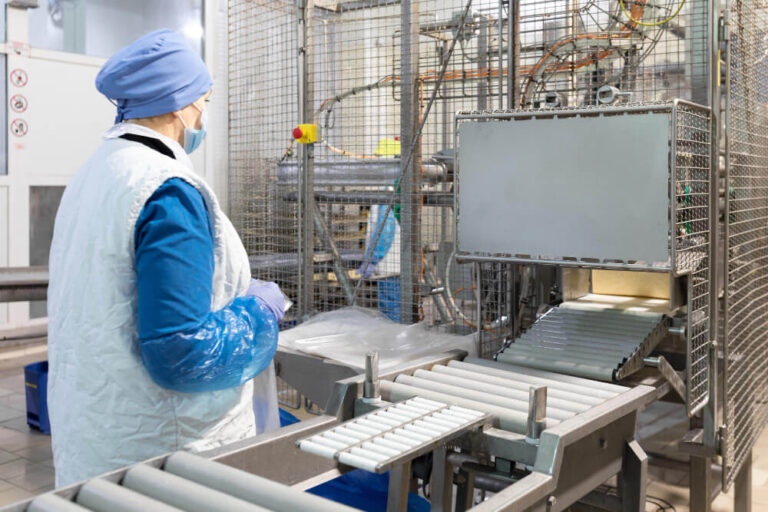
1. Meat and Meat Processing Facilities
- Portioned meat handling
- Pre-packaging transfer
- Processing lines
2. Dairy Products
- Cheese production
- Milk and yogurt processing lines
- Filling and packaging processes
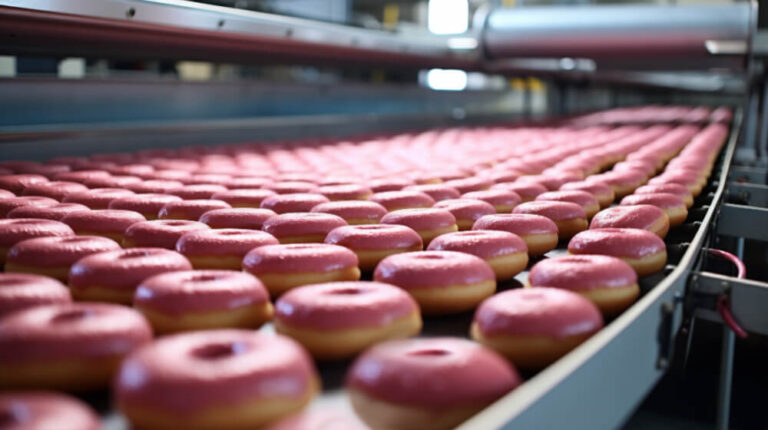
3. Bakery and Confectionery
- Bread production lines
- Biscuit and cake production
- Cooling and packaging processes
4. Nuts and Confectionery
- Turkish delight production
- Chocolate and candy production lines
- Packaging feeding systems
5. Frozen Food Production
- Cold environment resistance
- Product transfer systems
- Packaging lines
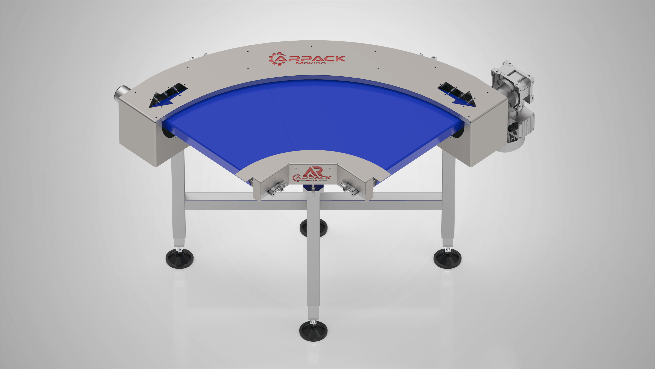
Belt-Type Stainless Steel Conveyor Systems
One of the most widely used systems in food production.
Advantages:
- Continuous product flow
- High transport capacity
- Compatibility with packaging machines
- Safe handling of delicate products
In particular, belt-type stainless steel conveyor systems for food production form the backbone of production lines.
Modular Belt Stainless Steel Conveyor Systems
Preferred in facilities with high hygiene requirements.
- Easy disassembly and cleaning
- Long service life
- Food-contact safe surfaces
- High hygiene standards
In particular, modular belt stainless steel conveyor manufacturing is one of the most preferred solutions in modern food facilities.
Advantages of Stainless Steel Conveyor Systems
1. Food Safety
Protects products from external contamination.
2. High Durability
Provides long-lasting performance under harsh production conditions.
3. Easy Cleaning
Reduces production downtime.
4. Production Efficiency
Automated transport increases production speed.
5. Low Maintenance Cost
Durable materials reduce failure rates.
What to Consider When Choosing a Conveyor Manufacturer for the Food Industry
Choosing the right manufacturer is critical for long-term success.
- Experience in the food industry
- Knowledge of hygienic design
- Custom project capability
- Local production and service network
- Reference projects
- Automation integration capability
In particular, selecting a stainless steel conveyor system manufacturer for the food industry directly impacts production line efficiency.
Industry 4.0 and Smart Food Production Lines
In modern food facilities, conveyor systems are no longer just transport equipment, but also data-generating automation components.
- Sensor-based control
- Production line monitoring
- Energy optimization
- Predictive maintenance systems
- PLC integration
This allows both hygiene and efficiency to be optimized simultaneously.
Stainless Steel Conveyor Solutions for the Food Industry by Arpack Machinery
At Arpack Machinery, we design and manufacture stainless steel conveyor systems for the food industry, modular belt conveying lines, and integrated production solutions. We develop custom projects for each production line to achieve maximum efficiency and hygiene standards.
From our production facility in Esenyurt, Istanbul, we provide manufacturing, installation, and delivery services not only in Istanbul but across all regions of Turkey.
To make your food production line more hygienic, efficient, and sustainable, you can contact the expert team of Arpack Machinery.